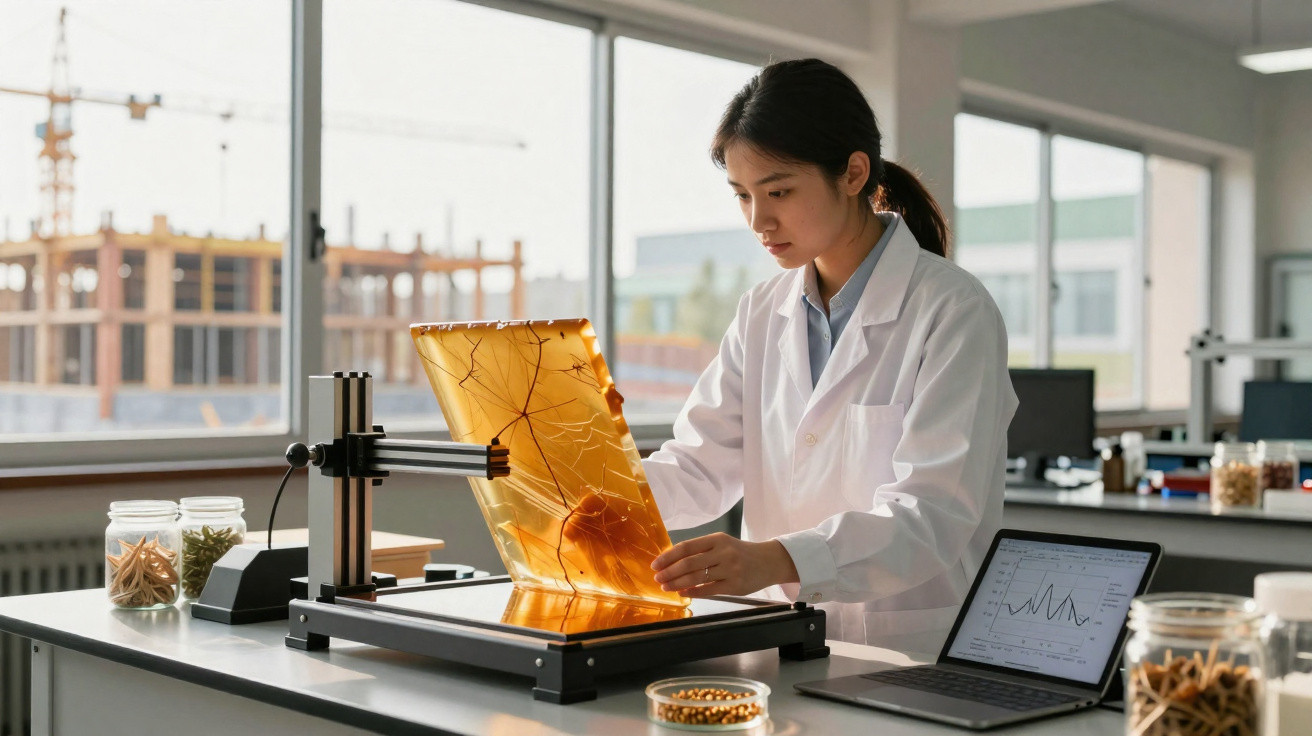
Cheap, hard-wearing and ubiquitous, plastic poses a straightforward yet weighty challenge for the sector: can a bio-based substitute deliver the same strength and consistency without the environmental burden?
The laboratory carries a light scent of pine and solvent, a sharp cleanliness that catches at the back of the throat. A universal testing machine gives off the low drone of a faraway train. Its grips hold a pale green composite strip, innocuous in appearance until it breaks with the taut crack of a violin string. Technicians speak in abbreviations-Tg, creep, D6866-as sample trays wait in rows like orderly tiles in a builders’ merchant. On the bench, a silver UV chamber shines as though the resin were sunbathing ahead of its test. A clipboard is tapped, while the drop-test tower sends a thud through the floor. I find myself counting each impact. The room then falls quiet as a fresh plate moves beneath the load cell. A number appears on the screen, prompting three people to smile. Something is coming together.
What a green resin must withstand
In this laboratory, a plant-based resin must endure the same punishing initiation as its petroleum-derived relatives. It is stretched in tension until necking begins, crushed in compression until it gives way, and flexed in three-point bending until the fibres murmur, then fail. Water immersion and freeze–thaw cycles make it expand and contract. A weathered rig recreates life when fixed to a façade, trembling through daily temperature changes. There are no concessions. If it cannot accept a screw without splitting or support a load in summer rooftop heat, it is rejected.
One morning, a batch labelled “L-47”-a lignin-epoxy containing a small amount of hemp fibre-produced a quietly impressive run. Its tensile strength approached the mid-60 MPa range, edging beyond commodity HDPE. After a gradual bake at 120°C, its flexural modulus came in at about 3 GPa, earning a restrained whistle from the rear of the room. Those same specimens completed 500 hours of UV exposure and returned only slightly paler. It was not flawless, but it was encouraging. We have all seen an underestimated project reveal real capability.
The reasoning behind those figures is built in layers. Plant oils and lignin supply carbon from farms and forests; epoxidation and anhydride curing transform them into a dense crosslinked network. Fillers such as milled straw reduce weight and cost, while fibres including flax or basalt bear the load. Dynamic mechanical analysis establishes the glass-transition range-perhaps 95 to 110°C-revealing how the material will behave on a black roof in July. Creep testing exposes the unwelcome reality of sagging. Bio-content is verified through ASTM D6866, ensuring that a “green” claim is supported by more than good intentions.
The construction-grade strength testing process
This is the process the team uses to turn liquid resin into construction-grade strength. Resin and hardener are first measured to the nearest gram, heated until they flow like honey, then vacuum-degassed to remove hidden bubbles. Fibres are cut, dried in advance and layered with enough resin to wet them fully without saturating them. The lay-up enters a heated press and cures under pressure for a count that feels interminable. Once post-curing is complete, the panel finally reaches the saw, which cuts it into dog-bone specimens and tidy bars with rounded edges.
Next comes the full test programme: tensile testing on an Instron, three-point flexural testing at 2 mm/min, Charpy impact testing for brittleness, and DSC/TGA to assess heat behaviour and decomposition. Water absorption is measured after 24 hours, 7 days and 30 days. Fire performance is examined with UL-94 and a small-scale cone calorimeter that records heat release. It resembles marathon training at accelerated speed. Honestly, no one carries out all of that every day.
The strongest laboratories communicate plainly. They do not conceal failures. One panel distorts; another absorbs excessive water; a third performs brilliantly in strength testing but creeps under a modest, persistent load at 60°C. Then somebody adjusts the cure programme by twenty minutes, and the outcome shifts.
“We’re not chasing the one hero number,” a senior tech tells me, hands in pockets. “We’re building a profile that a contractor can bet a warranty on.”
- Target tensile: 55–75 MPa for structural plastics replacement.
- Tg above 100°C for roof and façade service.
- Water uptake under 1.5% after 30 days to keep dimensions honest.
- Euroclass B-s1,d0 target with mineral flame-retardant fill.
- Bio-content verified at 55–70% by ASTM D6866.
The gap between laboratory and building site
Moving from a pristine bench to a dusty building site requires another set of capabilities. The resin has to operate on established production lines-extrusion for trims, pultrusion for profiles and injection moulding for clips-without blocking screws or smelling of salad dressing. Pigments must provide coverage at low loading, and the surface must accept a bead of sealant as readily as PVC. Near the door sits a basic click-fit rig, where profiles are repeatedly snapped together, bent and released. If installers struggle with the product on a scaffold with cold hands, the material has failed before the first invoice is issued.
The usual setbacks can be minor in appearance yet severe in effect. Moisture in fibres creates voids: attractive samples that fail prematurely. Excessive curing can make the interface brittle and allow cracks to take over during impact. Add too much mineral filler to secure a higher fire classification, and screw retention drops dramatically. The laboratory teaches compromise rather than wishful thinking. The first field trials will certainly uncover surprises. That is not a failure; it is the cost of learning about a new material.
Cost adds another burden to every test rack. Petroleum resins fluctuate with oil prices; plant-derived inputs fluctuate with weather and harvests. Some batches approach a commodity PP price point, while others remain more expensive until production volume increases. Flame retardants, UV packages and biobased plasticisers alter the calculation by pennies that matter. Nobody wants a greener bill that sinks a bid. One understated measure becomes especially valuable here: embodied carbon per kilogram. When a façade panel halves its footprint without surrendering years of service life, buyers begin calculating over the longer term-considering reputation, compliance and penalties they will avoid.
Who is backing plant-based resin-and why it could last
The people in this laboratory are not pursuing a press release. They want a specification sheet that allows a project manager to stop asking whether it works and begin asking how many pallets should be delivered. That requires independent reports, EPDs and fire ratings issued by organisations with no personal connection to the manufacturer. It requires the unglamorous achievement of passing an impact test in a cold chamber at 7 a.m., unseen by anyone. It also means identifying building components where replacing PVC, PP or ABS delivers the greatest benefit with the least disruption: soffits, rainscreen clips, window spacers, interior panels and cable trays.
A subtle cultural change underpins this work. The resin is not attempting to become miraculous; it is attempting to become ordinary. That is the real ambition. If it machines like PVC, bonds like epoxy and withstands a summer storm, the narrative moves from “eco” to “standard”. The drop-test tower becomes less of an attraction and more of a routine weekly task. The reward extends beyond any one product range: a way to reduce carbon without rewriting the building-site playbook.
What remains with me is how unremarkable the future appears once it functions properly. It is not a science-fiction façade or a timber cathedral on a magazine cover. It is simply a crew in hi-vis clothing fitting profiles that do not smell, do not warp and do not make landfill seem uneasy. The route from plant to panel is untidy, and the resin sometimes moves backwards. Yet when the data builds up and the components fit together, the question reverses. Perhaps plastic is not the default. Perhaps it is merely what we used until something better came through the laboratory door.
| Key point | Detail | Why it matters to the reader |
|---|---|---|
| Mechanical performance | Tensile 55–75 MPa, Tg ~100°C, low creep under heat | Understand whether the material can replace PVC/PP without unwelcome surprises |
| Durability in real conditions | UV 500–1000 h, low water absorption, targeted fire class | See how the material performs on façades and roofs |
| Impact and cost | 55–70% bio-content, reduced carbon footprint, volume-related costs | Assess ROI beyond the price per kilogram alone |
Comments
No comments yet. Be the first to comment!
Leave a Comment